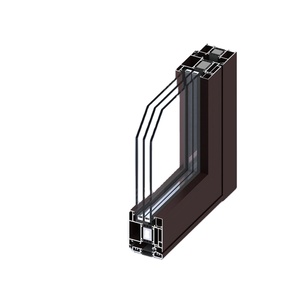
Direct factory procurement of structural aluminum extrusions, typhoon-tested storm shutters, acoustic bifold installations, and high-impact glazing accessories engineered for severe environmental thresholds.
Operating continuously since 1973 with over five decades of mechanical precision, our integrated manufacturing lines eliminate intermediary trading risks. We provide architectural firms, large commercial contractors, and system distributors with end-to-end engineering traceability.
Unlike regional suppliers who incorporate unchecked post-consumer scrap, our structural shutter slats and window subframes rely strictly on virgin A00 aluminum ingots. Extruded with strict wall-thickness tolerances compliant with EN 755-9 and ASTM B221, ensuring uncompromised mechanical tensile strength under violent dynamic cyclic deflection.
Our storm shutter assemblies undergo rigorous testing under ASTM E1886/E1996 Large Missile Impact and TAS 201/202/203 criteria. Retaining flawless interlocking stability under wind gust pressures exceeding 4,500 Pa, our storm systems safeguard luxury residential compounds, data hubs, and critical infrastructure against severe typhoon vectors.
Roller shutters positioned in harsh coastal or tropical latitudes require superior surface treatment. Our multi-stage automated pre-treatment bath combines chrome-free passivations with Qualicoat Class 2 certified AkzoNobel powder and fluoropolymer PVDF coatings, resisting salt fog corrosion for over 3,000 continuous hours (ASTM B117).
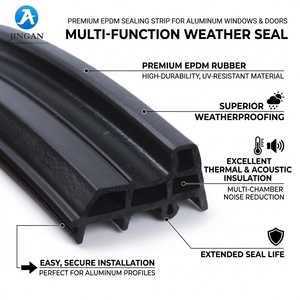
For custom architectural fenestrations, our proprietary CNC tooling facility mills bespoke extrusion dies in as little as 10 to 14 business days. Whether matching complex brick-mold setbacks, hollow thermal-break cavity profiles, or custom EPDM inlaid weather-stripping channels, our design team translates architectural CAD/BIM specifications directly into reality.
Modern luxury developments demand high sound attenuation. Our polyurethane-injected micro-perforated slats, paired with reinforced brush rails and synthetic rubber gaskets, deliver an acoustic reduction factor of up to Rw 34 dB. Urban traffic, ambient flight path rumble, and intense downpours are mitigated before entering the interior envelope.
Drive engineering sits at the core of our motorized shutters. We integrate tubular drive motors compatible with Zigbee 3.0, Matter, RS-485 Modbus, and dry-contact building automation systems (BMS). Our silent-running motor units include thermal overload sensors, obstacle auto-reverse safety stops, and battery backup fail-safes during brownouts.
Understanding the exact technical division between Contract Manufacturing (OEM) and Original Design Co-Development (ODM) allows procurement departments to optimize tooling investments, component lead times, and structural warranties.
| Evaluation Parameter | OEM (Contract Extrusion & Sourcing) | ODM (Turnkey Engineered Systems) | Testing & Compliance Standards |
|---|---|---|---|
| Primary Billet Alloy | Aluminum 6063-T5 to client-provided drawings | Custom structural 6063-T6 or 6005A structural alloy | ASTM B221 / EN 573-3 |
| Slat Wall Thickness | 0.8 mm – 1.2 mm single/double skin | 1.4 mm – 2.5 mm reinforced hurricane extrusions | ISO 9001 / Micrometer Verified |
| Insulation Injection | Polyurethane foam (45 kg/m³ density) | High-density PU foam (up to 75 kg/m³) or Aerogel | DIN 4102 B2 Fire Rating |
| Motor & Drive Options | Standard mechanical limit tubular motors | Brushless electronic obstacle-detection motors + BMS | CE / UL / TUV Recognized |
| Wind Pressure Limits | Class 2 to Class 4 (EN 13659) | Class 5 to Class 6 (Resisting up to 180 mph gusts) | TAS 202 Static / TAS 203 Cyclic |
| Surface Protection | Architectural Class 1 Powder Coating (60–80 µm) | Fluoropolymer PVDF 3-Coat or Hard Anodizing (25 µm) | AAMA 2605 / Qualicoat Seaside |
| Tooling & Mold Turnaround | 12–15 Days from client DWG approval | 20–25 Days with finite element FEA stress analysis | Full CMM Dimensional Report |
Our Massachusetts manufacturing facility and affiliated extrusion yards minimize hand-offs. Traditional sourcing chains fracture accountability between the profile extruder, the PU-slat foaming specialist, the powder coater, and the tubular drive supplier. We house these stages under a unified quality assurance regime.
"Procurement directors often overlook thermal bridging along headboxes. When designing our insulated thermal roller shutters, we engineer poly-structural thermal breaks between the exterior fascia and the interior architectural reveal. The result is a total window-assembly U-value reduction of up to 32% during winter peak load conditions."
Supply chain shocks, building decarbonization mandates, and extreme weather frequencies are shifting how developers and commercial contractors evaluate shutter supply contracts. Incorporate these four foundational macro developments into your sourcing strategy.
Global import restrictions such as the EU's Carbon Border Adjustment Mechanism (CBAM) are transforming material compliance. Forward-thinking suppliers leverage hydroelectric smelters generating primary billets with under 4.0 kg CO2 per kg of finished aluminum, shielding commercial projects from cross-border carbon tariffs.
Modern building designs are moving away from solid opaque security slabs. Demand is growing for laser-perforated and slotted articulated slats that admit indirect diffused daylight while filtering 85% of solar infrared radiation, reducing building HVAC chilling loads without sacrificing physical intrusion resistance.
Building Integrated Photovoltaics (BIPV) are expanding into motorized exterior envelope closures. Slat profiles embedded with thin-film monocrystalline solar cells feed decentral low-voltage battery storage, operating the shutter drive motors independently of the municipal grid.
Proprietary radio-frequency remotes are giving way to open IoT topologies. Tier-1 real estate builders require motor controllers natively compatible with Apple HomeKit, Google Home, and commercial Crestron systems via Thread-mesh low-latency networks without third-party converter boxes.
With insurance underwriters tightening requirements along coastal hurricane corridors, demand for basic unrated shutters is falling. Specifiers now mandate dual-locking anti-lift end-locks and heavy steel spring retainers capable of surviving cyclical positive and negative pressure inversions without rail track pop-out.
Developers avoid fragmented trade disputes by purchasing complete architectural fenestration packages—including aluminum curtain walls, soundproof casement windows, EPDM sealing gaskets, and matching exterior motorized shutters—from a single OEM factory.
In-depth responses covering custom tooling investments, wind load testing, minimum order quantities, and international logistics standards.
For custom proprietary slat profiles or bespoke architectural guide rails requiring new steel extrusion dies, our typical minimum order is 500 kilograms per profile section. When ordering complete factory-assembled shutter units, our baseline project volume begins at 20 sets for multi-family residential or commercial fenestration projects. In-stock structural dies carry no tooling charges.
Our assemblies are tested under ASTM E330 (structural wind load), ASTM E1886/E1996 (missile impact & cyclic pressure), and European standard EN 13659 Class 6 specifications. In our on-site pressure chambers, assemblies undergo static pressure cycles simulating wind velocities up to 180 mph (290 km/h) without structural slat failure or track derailment.
Yes. Our automated electrostatic lines apply Qualicoat Class 1 and Class 2 finishes across the full RAL Classic color spectrum. For severe maritime conditions, we offer Qualicoat Seaside-level acid pre-treatment or architectural Class I anodizing (20 to 25 microns), rated for 3,000+ hours in continuous neutral salt spray (ASTM B117) testing.
We supply turnkey systems incorporating industry standard drives such as Somfy, Dooya, and customized OEM brushless DC motors. Supported automation protocols include dry-contact relays, RS-485 for KNX/Crestron commercial building management systems, 433 MHz bi-directional RF, and native Zigbee 3.0 / Matter systems with remote mobile app synchronization.
Finished roller shutter curtains are interleaved with protective protective film, wrapped in heavy-duty pearl cotton foam sleeves, and packed in reinforced honeycomb cardboard or heat-treated ISPM 15 export wooden crates. Structural guide tracks and box housings are bundled with internal corner edge guards to prevent transit rub and transit abrasion across multi-modal container freight.
For standard architectural profiles and catalog colorways, lead time is 18 to 22 business days following CAD sign-off and deposit receipt. Projects involving custom die extrusion tooling require an additional 10 to 14 days for steel die production, initial test extrusions, and dimensional sample dispatch via international air express.